
 By Coco
Understand the sand-system checks behind consistent molds, not just the low tooling cost.
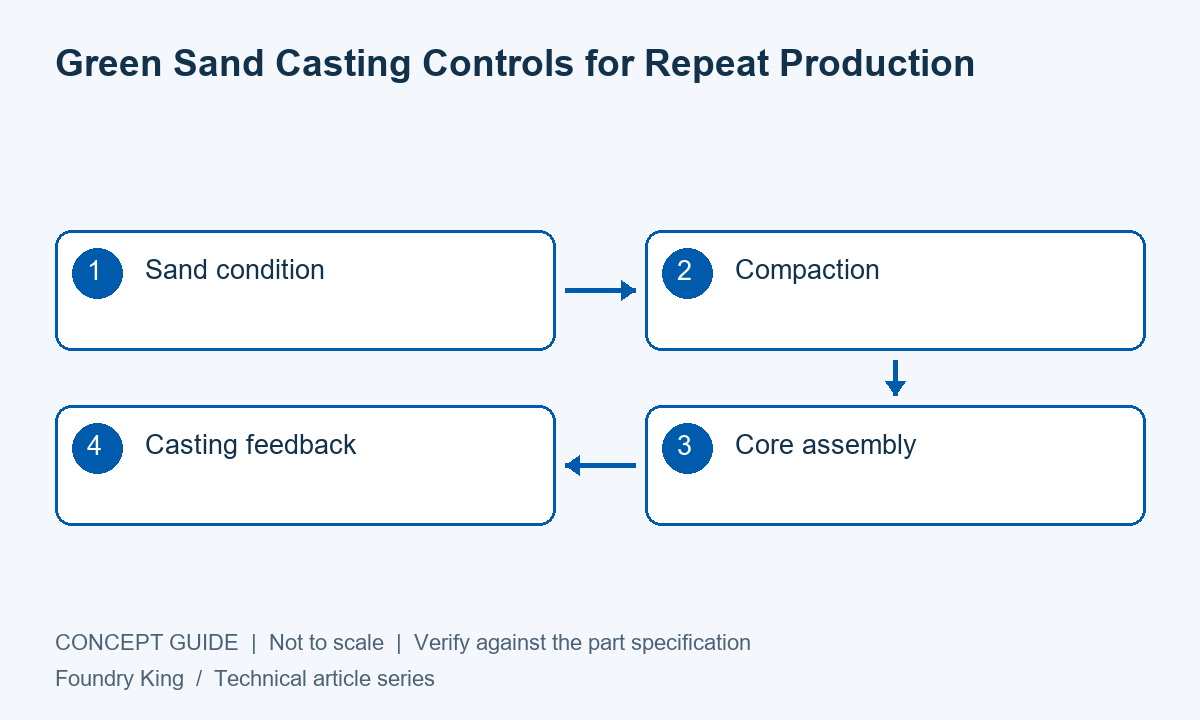
Green sand casting controls connect the behavior of a reusable molding sand to the quality of the finished component. “Green” describes the mold’s moist, unbaked condition, rather than a claim that the process has no environmental impact. For repeat orders, control of the sand system and molding equipment matters as much as the approved pattern.
Balance strength and permeability
A green sand mixture normally combines sand, clay-based binder, water and route-specific additives. Too little usable strength can lead to mold damage or erosion; an unsuitable combination of moisture and permeability can contribute to gas-related defects. These factors must be assessed as a system rather than corrected independently by adding more water or binder.
Ask how the foundry monitors its circulating sand and what happens when results move outside its operating limits. Test records are useful only when linked to corrective actions. A single laboratory value supplied with a sample does not show that a production sand system remains stable across shifts.
Make compaction repeatable
Mold hardness and density affect shape, handling and the interaction with molten metal. Inconsistent ramming can leave weak areas around deep pockets or create uneven behavior across the mold. Pattern layout, machine settings and the condition of flasks and alignment features influence this repeatability.
The relevant question is whether the selected molding line can reproduce the proposed part. A pattern designed for one line may need changes before it is moved to another. Treat such a transfer as a method change requiring review, particularly when wall thicknesses and alignment are critical.
Protect the core and parting line
Cores are often produced using a different binder system from the mold. Their gas generation, strength and location therefore require separate attention. Provide clear limits for internal passage alignment, accessible cleaning and minimum functional wall thickness, rather than measuring only the outside envelope.
At the parting line, poor alignment can create mismatch. Subsequent grinding may improve appearance without correcting the underlying dimensional error. Agree where mismatch is measured, what is acceptable and whether it affects the later machining setup.
Use defects as diagnostic evidence
| Observation | Possible area to investigate | Do not conclude automatically |
|---|---|---|
| Sand inclusions | Mold erosion, handling or cleaning | That the alloy heat was wrong |
| Gas-related cavities | Moisture, cores, venting and filling | That one sand test explains every pore |
| Repeated mismatch | Alignment, pattern seating or mold assembly | That grinding restores the geometry |
Approve a representative production route
Request samples made with the intended tooling, molding equipment and finishing sequence. A hand-prepared sample can answer a feasibility question without proving production-line capability. Record any differences between trial and production methods so that acceptance is based on comparable evidence.
For stable repeat supply, retain the approved pattern identification and revision, material specification and critical checks. When a defect trend appears, compare results by batch and location. That makes it easier to distinguish a general sand-system issue from a localized problem in gating, core support or part geometry.
Frequently asked questions
Is green sand restricted to iron castings?
No. Foundries use green sand with different ferrous and nonferrous alloys. Actual capability depends on the equipment, sand system and specific foundry practice.
Does reusable sand mean molds are reusable?
The mold is broken to remove the part. Much of the sand may be conditioned and reused, but the individual mold cavity is expendable.
Discuss your component requirements
For related information, review compare casting material families, or review a repeat-production requirement. Include the drawing revision, alloy, quantities and critical acceptance requirements so the proposed route can be reviewed against the actual part.

Get Premium Casting Products
Join foundryking.com Newsletter to get more information of different premium OEM Casting products in China.


