
 By Coco
Measure the work needed to reach the finished part from each starting form.
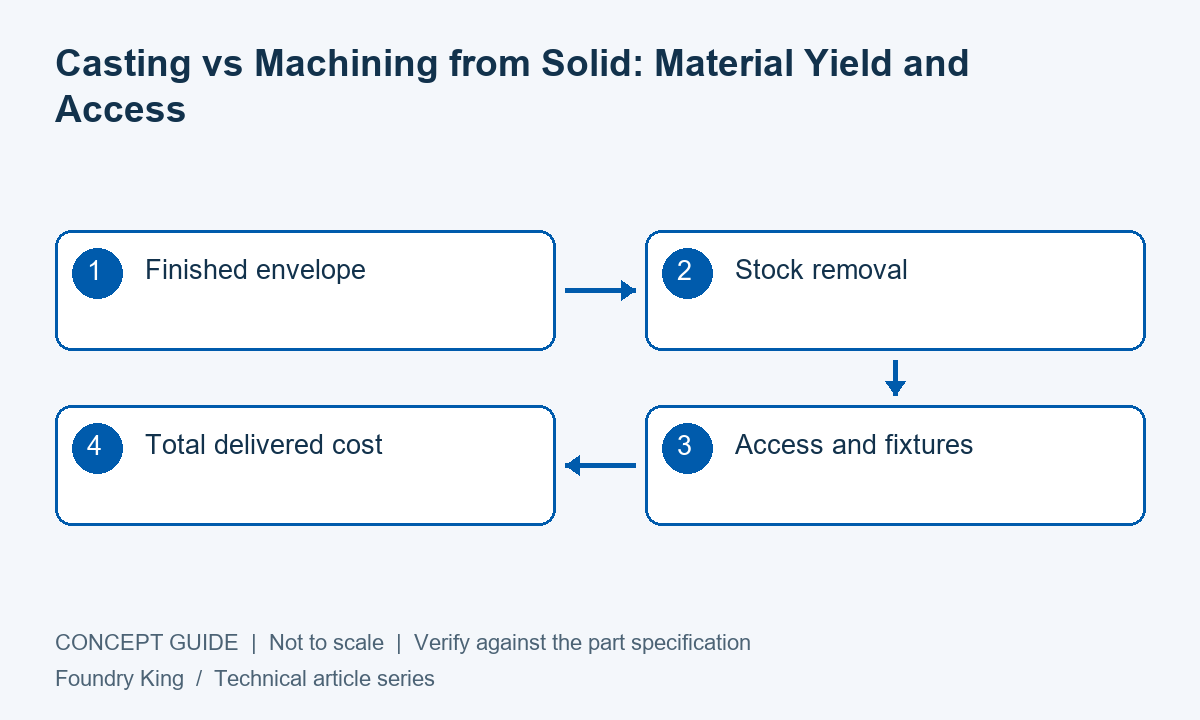
Casting vs machining from solid is often decided by the relationship between the finished shape and the starting material. A compact part with simple accessible features may suit billet or bar stock. A hollow body with several bosses may remove far more material and require a more complicated machining route. Compare those actual operations before choosing a blank.
Calculate material use realistically
Estimate the stock envelope and the mass remaining in the finished part. Then include cutoff losses, gripping stock and any additional material required for multiple setups. The difference is not automatically waste cost because recoverable scrap may have value, but it still represents purchased material and machining effort.
A casting also has nonproduct metal in its gating and feeding system, along with process losses. Do not compare a net casting weight against a gross billet purchase and assume the result captures the full economics. Use a cost model that consistently includes yield and recovery for each route.
Review tool access
Deep internal pockets, intersecting passages and enclosed cavities can require long tools, special operations or joining of separately machined pieces. Casting may form some of this geometry nearer to its final shape. However, cores and internal cleaning must be feasible, and critical surfaces may still need machining.
Identify the least accessible feature on the drawing. It can determine the preferred process more strongly than the outer profile. Ask the machinist and foundry to explain how that feature is made, inspected and cleaned in the final component.
Design the machining datum scheme
A casting needs repeatable locating surfaces and enough stock to clean up the required features. Billet machining needs its own fixture and setup sequence. Compare the number of operations, workholding changes and opportunities for accumulated error.
If the cast blank varies, a nominally shorter machining cycle can be offset by setup adjustments or rejected cleanups. Review sample variation and the relationship between the casting datum scheme and the final drawing. The lowest nominal cycle time is not necessarily the most repeatable route.
Compare the complete order
| Factor | Machining from solid | Near-net casting |
|---|---|---|
| Initial tooling | Workholding and cutting strategy | Pattern/tooling plus workholding |
| Internal shape | Limited by access and tool reach | Limited by core, cleaning and inspection route |
| Design change | May be relatively direct | May require tooling or method revision |
Use a break-even model carefully
Separate one-time and recurring costs. Model realistic order quantities and include first-article inspection, material certification, heat treatment and finishing. A break-even quantity is specific to the component and quotation assumptions; it should not be presented as a universal number for casting.
For uncertain demand, consider staged development. Machined prototypes can validate assembly, while casting development addresses future repeat supply. Document what each prototype proves, because a billet sample does not establish casting soundness or as-cast dimensional capability.
Frequently asked questions
Does near-net shape eliminate CNC machining?
Often not. It can reduce the amount of material removed while retaining machining for functional dimensions and surfaces.
Is a billet prototype representative of a cast production part?
It can support geometry and assembly checks, but material structure, defects and manufacturing variation may differ.
Discuss your component requirements
For related information, review machined component requirements, or compare starting-form options. Include the drawing revision, alloy, quantities and critical acceptance requirements so the proposed route can be reviewed against the actual part.

Get Premium Casting Products
Join foundryking.com Newsletter to get more information of different premium OEM Casting products in China.


